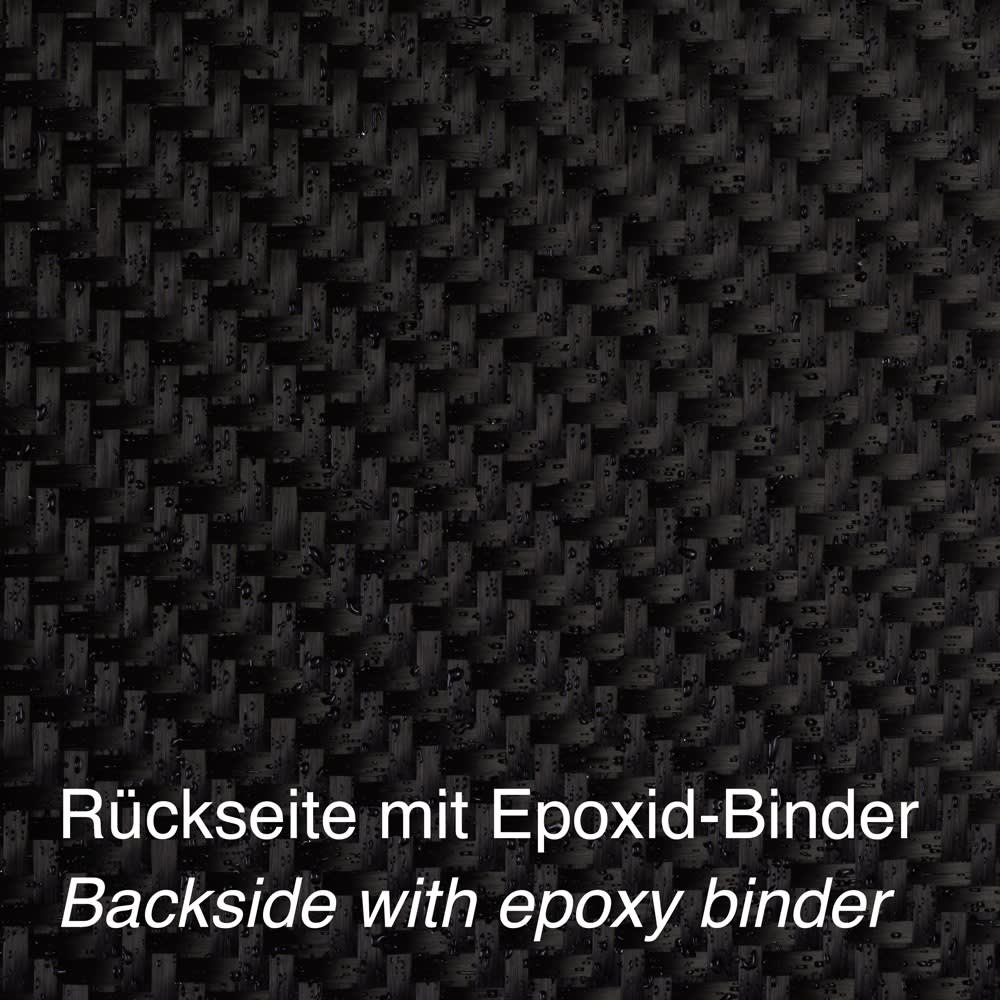
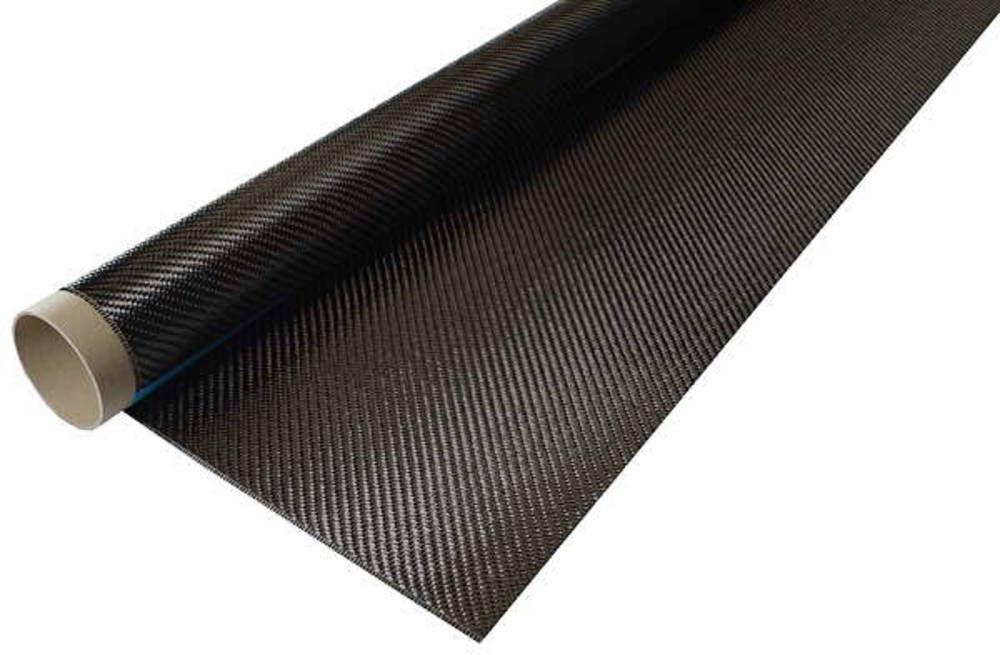
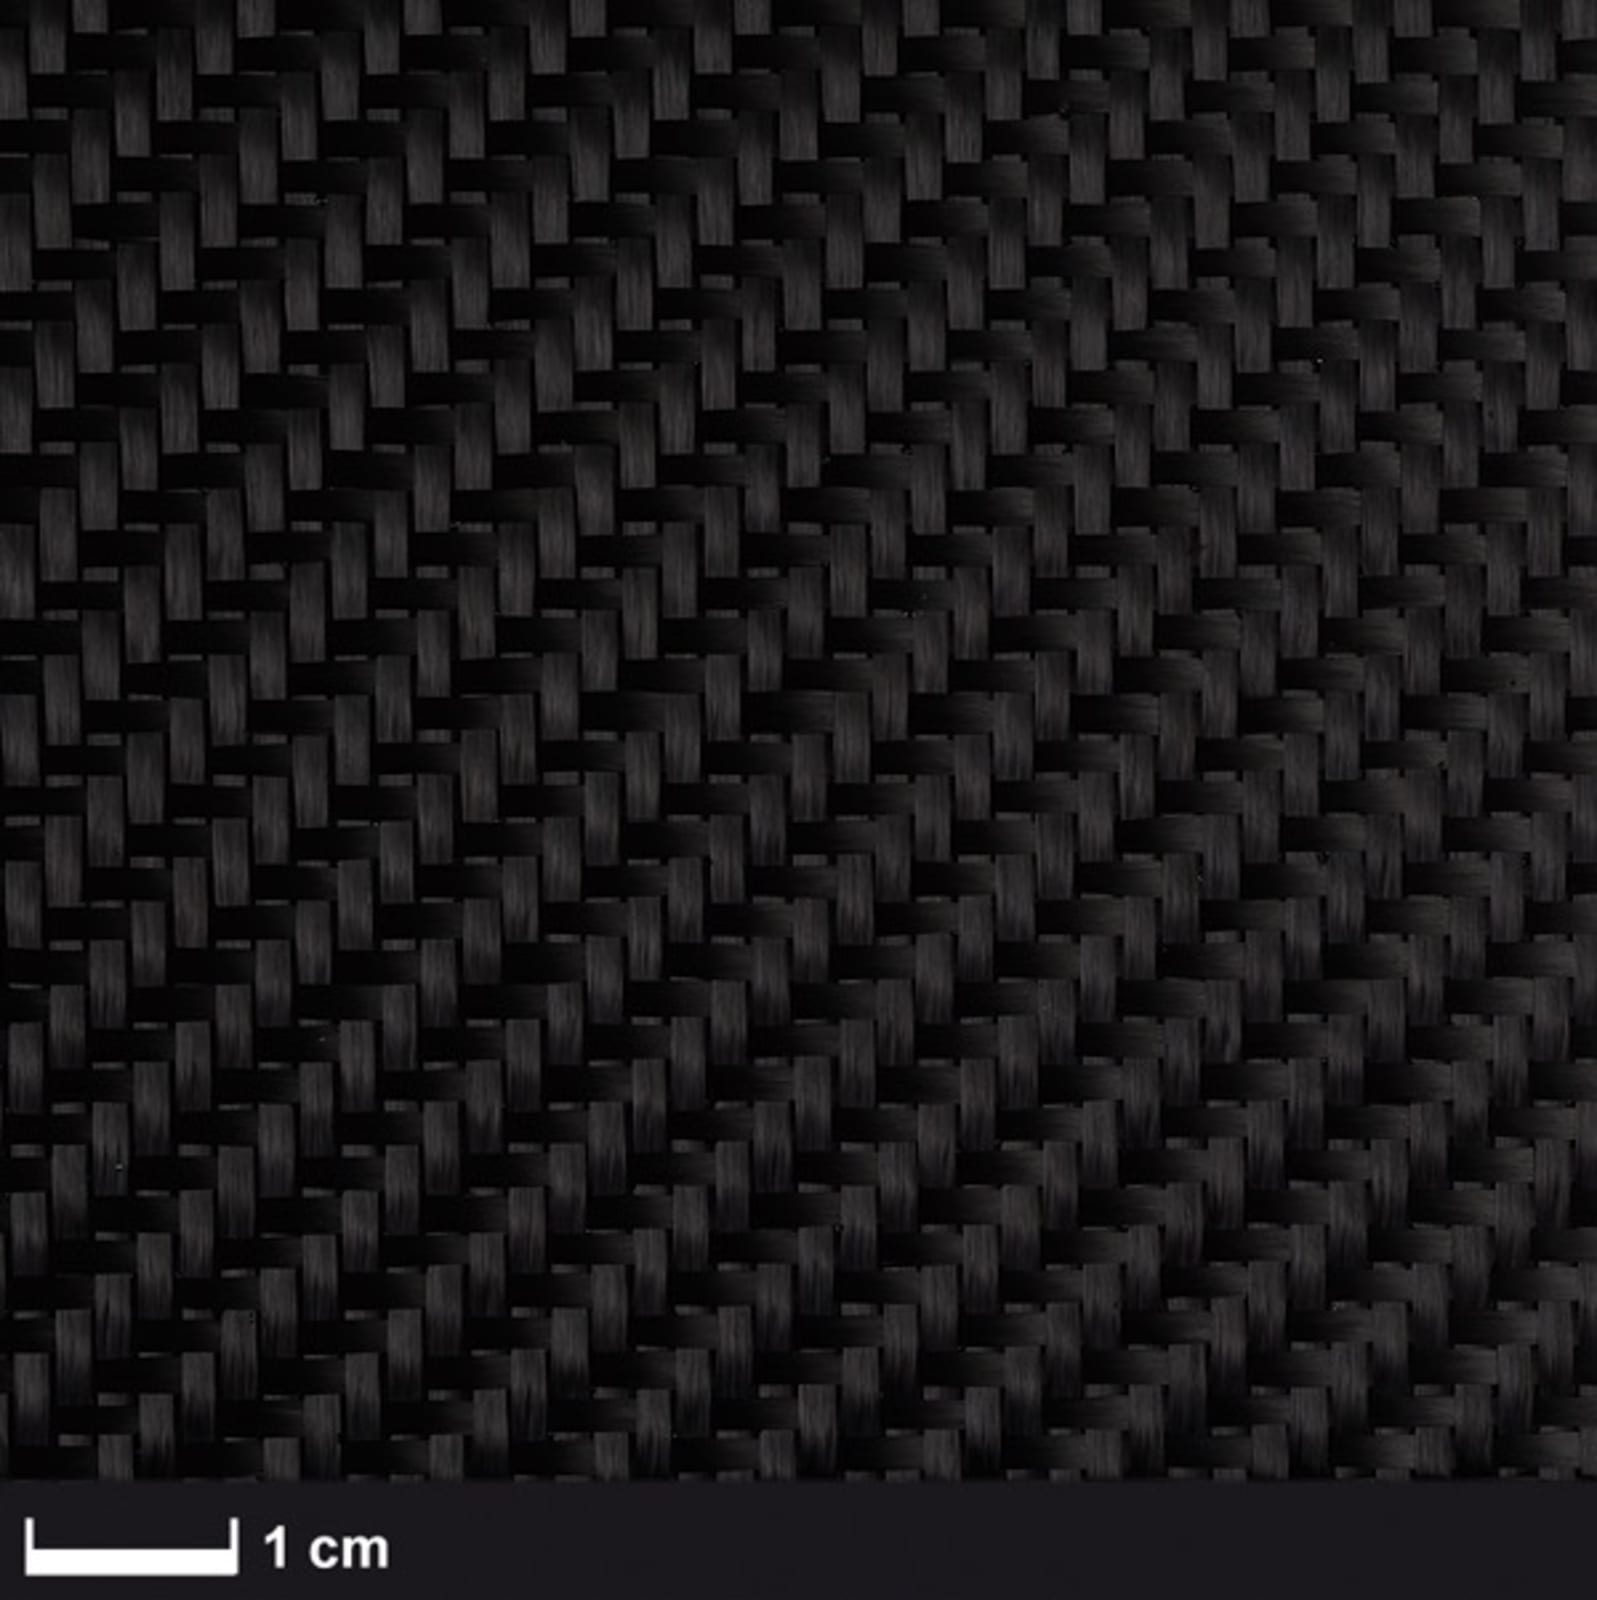
200 g/m² carbon fabric (Style 452-5 Aero) in a 2/2 twill weave, with a one-sided epoxy binder for improved yarn stability. For dimensionally stable cut pieces, heat-formable reinforcement plies and high-quality visible carbon components.
MATERIAL TO AEROSPACE SPECIFICATION
The fabric is manufactured from high-strength 3k carbon fibres with 5 ends/cm in both warp and weft. The one-sided epoxy binder stabilises the fabric construction, substantially reduces yarn fraying at cut edges and facilitates accurate positioning in multi-ply lay-ups. Heat can be used to preform the fabric to the required component shape before resin impregnation.
Technical data
| Fabric style |
Style 452-5 Aero, binder-stabilised |
| Fibre type |
Tenax® HTA 40 E13 or Pyrofil™ TR30S (HT, 3k) |
| Yarn linear density |
200 tex |
| Base carbon fabric weight |
200 g/m² (R&G nominal value) |
| Epoxy binder application |
approx. 10–15 g/m², one side |
| Areal weight incl. binder |
217 ± 11 g/m² (ECC specification) |
| Weave |
2/2 twill |
| Warp / weft count |
5.0 ± 0.2 / 5.0 ± 0.2 ends/cm |
| Fabric width |
100 cm (± 1 cm) |
| Finish |
One-sided epoxy binder for yarn stabilisation; smooth opposite side |
| Fibre specification |
WL 8.3611 |
Typical applications
- Dimensionally stable cut pieces and preformed reinforcement plies for CFRP parts
- Visible carbon components, fairings and body panels for motorsport
- Fuselage shells, wing components and fairings for model aircraft and UAVs
- CFRP shells and technical covers for boatbuilding and sports equipment
- Multi-ply laminates requiring accurate positioning of fabric cut pieces
Properties and processing
The one-sided binder treatment substantially reduces yarn displacement during cutting and handling. Heat can activate the epoxy binder, allowing the fabric to be preformed in a heated press tool or temporarily fixed to a suitable substrate. Preforming does not replace subsequent complete impregnation with laminating resin.
When using conventional hand lay-up without heat activation of the binder, place the smooth, binder-free side towards the final visible surface or corresponding mould surface. The discrete binder deposits can otherwise prevent full contact with the mould and cause small air pockets. Suitable epoxy laminating resin systems are recommended; ensure complete fibre wet-out and careful air removal.
Material selection
The Style 452-5 Aero carbon fabric without binder stabilisation is an alternative for conventional wet lay-up without an additional binder coating. The binder-stabilised version is particularly beneficial where cut pieces must retain their fibre alignment or heat-assisted preforming is required.
Calculated laminate data for hand lay-ups with 35% fibre volume fraction
The following R&G calculations are based on the carbon fabric weight of 200 g/m². The additional epoxy binder is not included.
| Calculated resin requirement |
approx. 241 g/m² |
| Calculated laminate thickness |
approx. 0.32 mm |
| Calculated laminate areal weight excluding binder |
approx. 441 g/m² |





 MSDS Carbon fibre (PDF)


